Bending without cracks
Restored ductility lets the element follow the radii on the drawing – the tube bends predictably and holds its geometry.
Since 1959
Tel. +90 312 814 51 20
WhatsApp +90 533 619 95 45
Email: t@tormec.com.tr
BALÇIK Isı Elemanları Sanayi Ticaret A.Ş.
Fatih Mh. Turgut Özal Blv. No:50
Kahramankazan 06980 Ankara Türkiye
Bright annealing
Rolling compacts the MgO and cold-works the sheath: the tube leaves the mill harder, under residual stress and less ductile. Annealing under a protective atmosphere reduces hardness and residual stress and restores ductility – without oxidising the surface.
It sits between rolling and forming: only an annealed tube can be bent to tight radii without cracking. The heat also drives residual moisture out of the MgO.
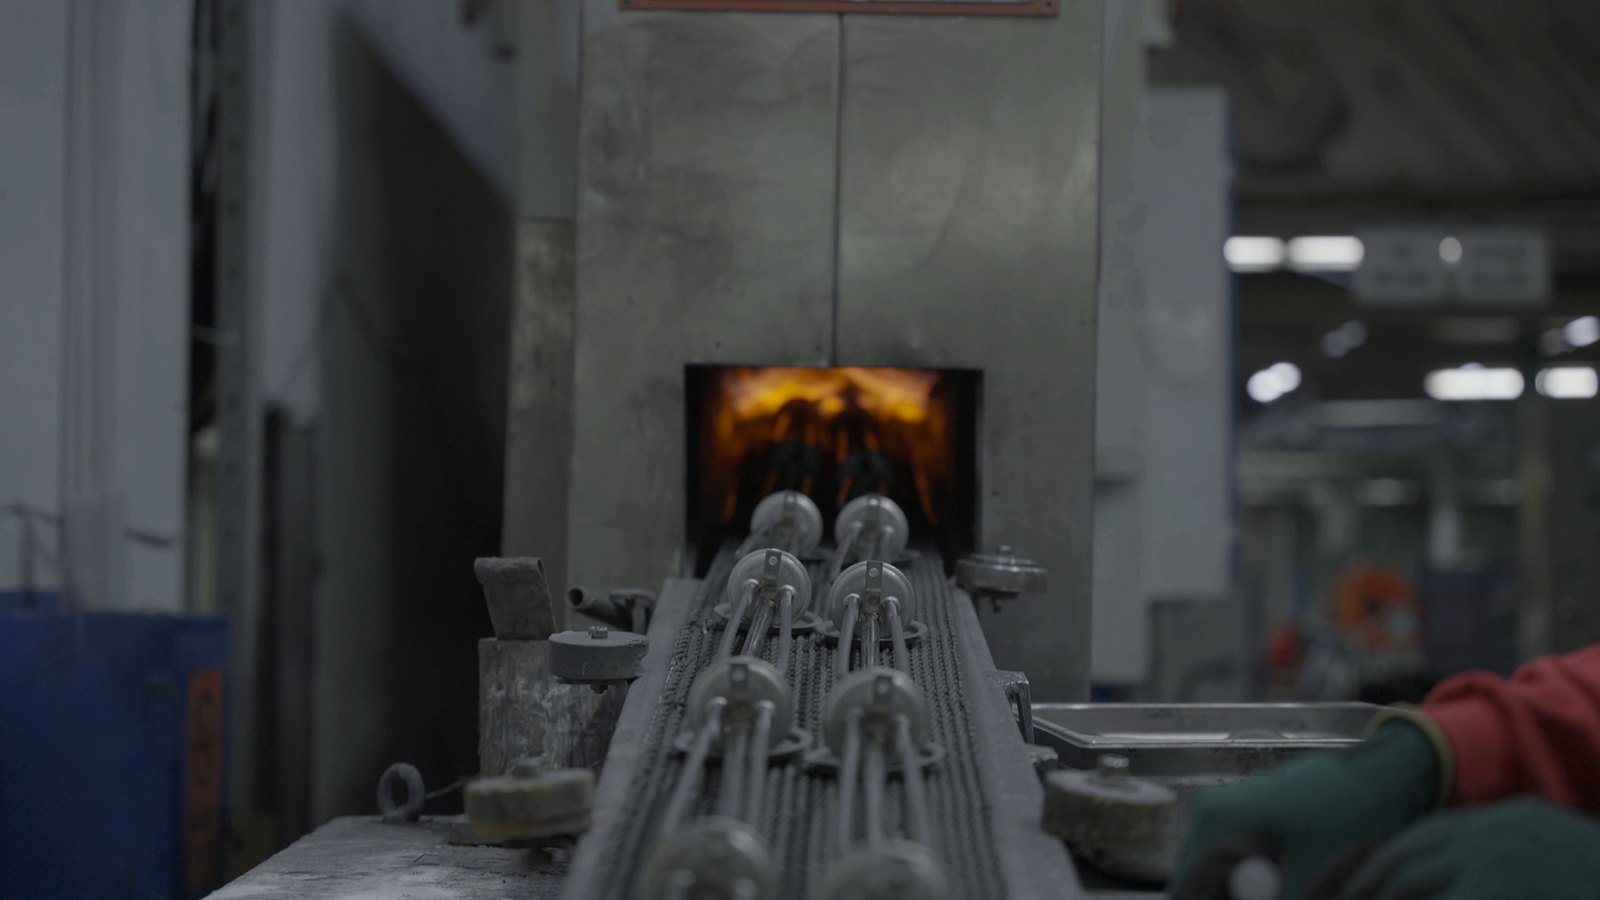
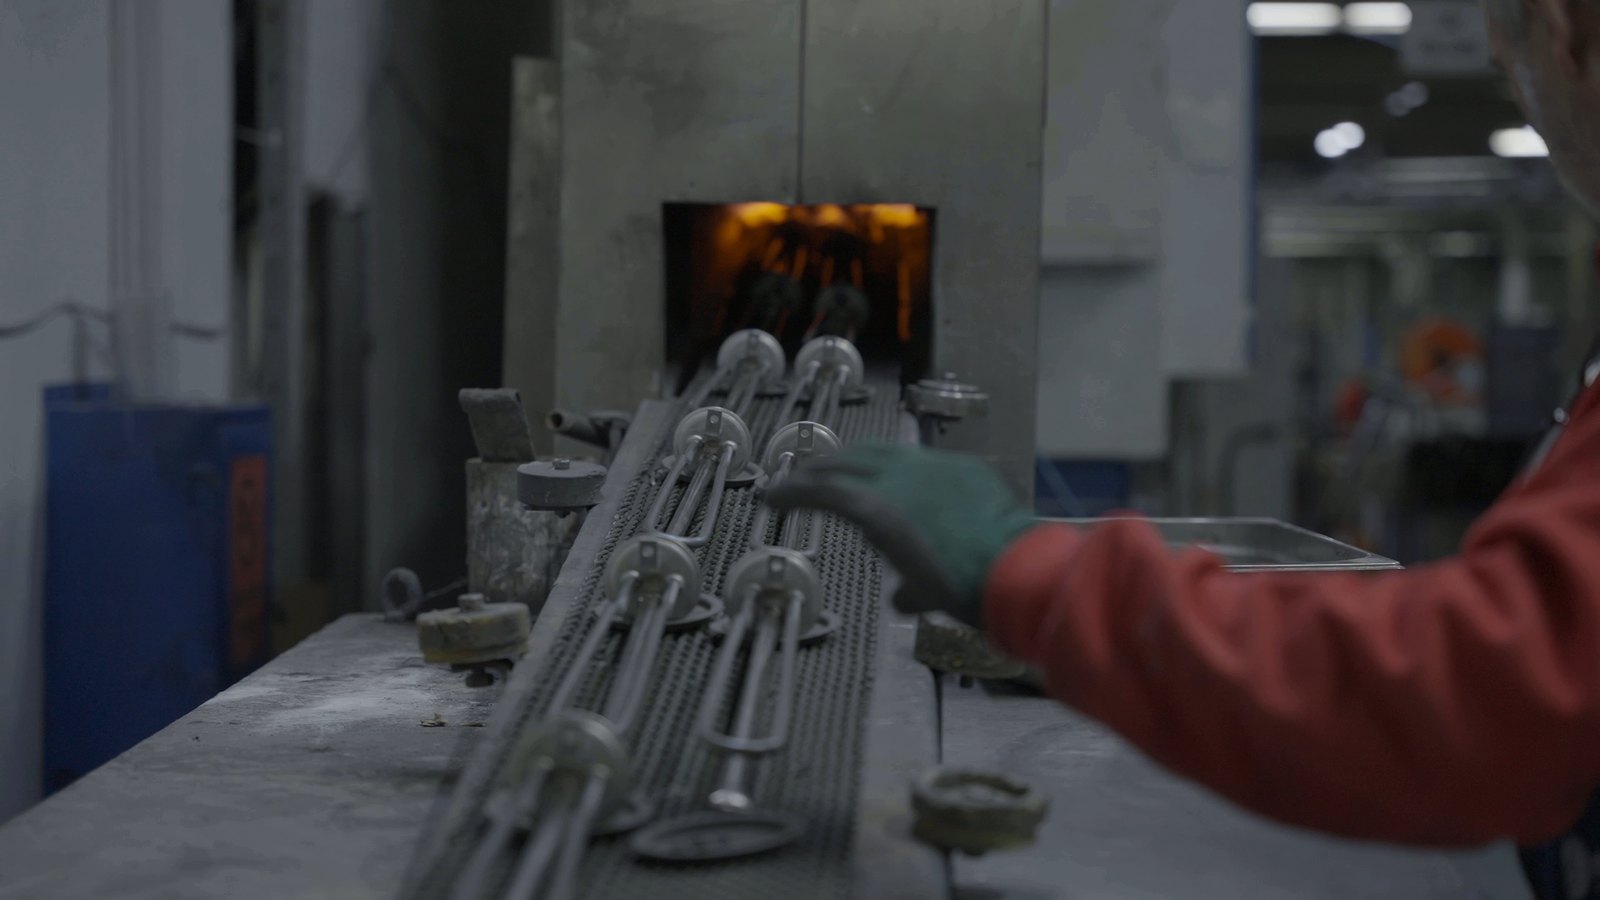
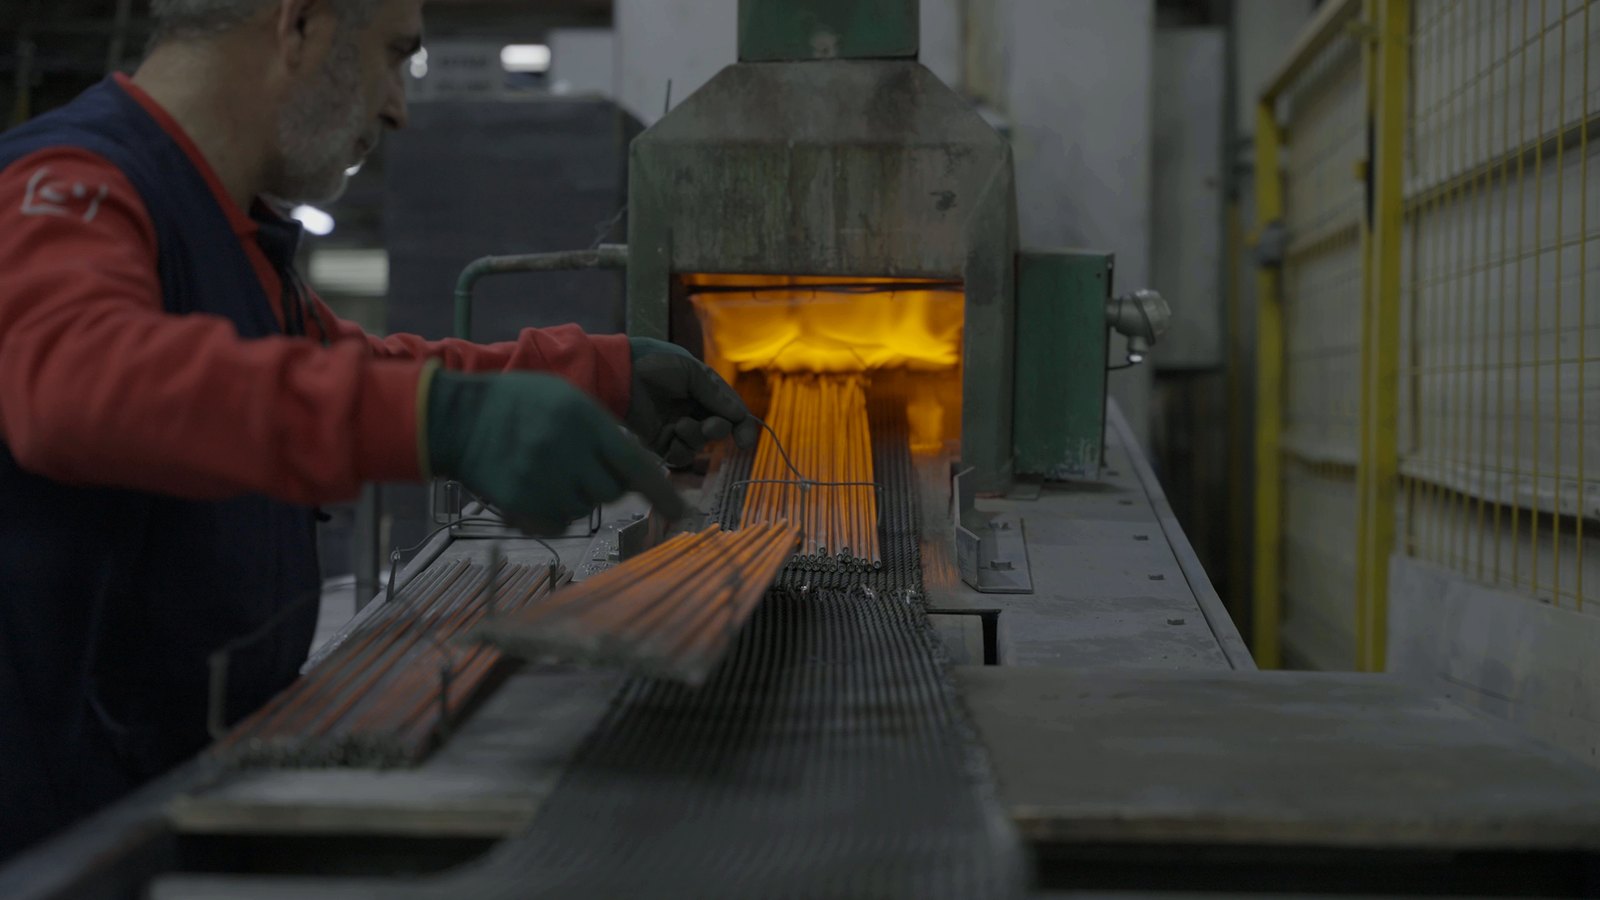 Annealing furnace
What changes
Annealing does not raise the strength of the tube; it makes it formable. The cold-worked structure recrystallises: elongation rises, hardness and residual stress fall.
| Property | After rolling | Annealed in air | Bright-annealed |
|---|---|---|---|
| Hardness and residual stress | High – cold-worked | Reduced | Reduced |
| Ductility for bending | Limited – tight radii risk cracks | Restored | Restored |
| Surface after the furnace | As rolled | Dark oxide scale, chromium-depleted beneath | Bright and oxide-free |
| Follow-up treatment | Anneal before tight bends | Pickling or mechanical cleaning | None required |
| Corrosion resistance at delivery | – | Restored only after pickling | That of the sheath grade |
| Brazing of fittings | – | Surface must be cleaned first | Clean surface, ready to braze |
The furnace
Hot stainless steel in air forms a dark oxide scale with a chromium-depleted layer beneath it. In a dry hydrogen-containing atmosphere (low dew point), at 1040 – 1100 °C for stainless sheaths, the conditions are reducing, so no oxide forms – and the tube cools under the same atmosphere before it leaves the furnace.
What it means for your element
Restored ductility lets the element follow the radii on the drawing – the tube bends predictably and holds its geometry.
No scale to flake off, no pickling residue: a uniform surface for visible elements and for brazing flanges and nipples.
Without scale and chromium depletion, the sheath delivers the corrosion resistance of its grade – no pickling needed.
Field evidence
We exposed conventionally annealed and bright-annealed tubes side by side for 12 months in a marine atmosphere – high temperature, salt and humidity. Afterwards each tube was split in half and its surface examined under an optical microscope.
Bright-annealed
Annealed in hydrogen at 1040 – 1100 °C and cooled rapidly under the same gas: no oxide layer to start corrosion from.
Conventionally annealed
Annealed in air, the sheath carries a dark oxide scale with chromium-depleted steel beneath – the weak point in a salty, humid atmosphere.
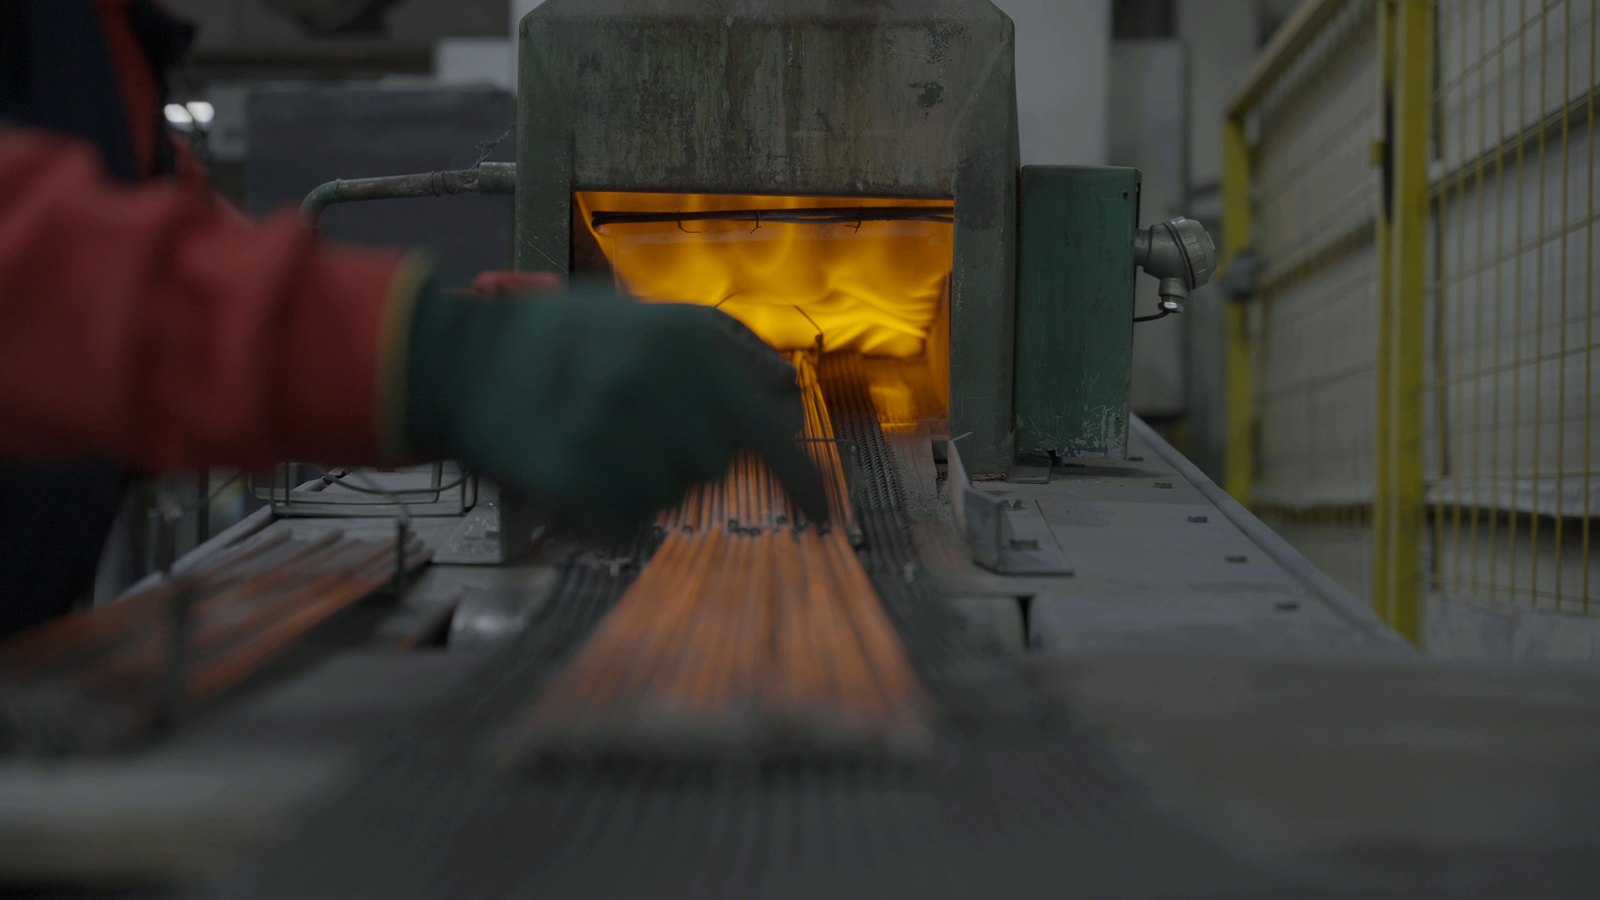
On our lines
Related
Send the drawing. We check bend radii, sheath grade and surface requirements and confirm the forming route before we quote.
Engineered and made in Ankara · since 1959
Three generations of know-how, our own welded tube and brazing lines, an engineering team with its validation laboratory and a 100 % electrical test on every element – so the heat inside your product is the one thing you never have to worry about.
Bright annealing reduces hardness and residual stress after rolling, restores ductility for bending and keeps the stainless sheath oxide-free – no pickling.
BALÇIK TORMEC designs and manufactures tubular heating elements in Kahramankazan, Ankara, since 1959 – series and custom production to your drawing, VDE-approved element families, ISO 9001:2015, exports to more than 60 countries.
Reception & switchboard
Human resources
Worldwide sales
Customers outside Türkiye – English, Russian, Arabic
Domestic sales – Türkiye
For customers in Türkiye · Türkçe
Purchasing & imports
Accounting
Quality
Production & planning
We use essential cookies to run the site and, with your consent, functional cookies for embedded maps and anonymous usage statistics (Google Analytics). No advertising or profiling cookies are used. See our Cookie Policy and KVKK / privacy notices.
Sitenin çalışması için zorunlu çerezleri; onayınızla gömülü harita için işlevsel çerezleri ve anonim kullanım istatistiklerini (Google Analytics) kullanıyoruz. Reklam veya profilleme çerezi kullanılmaz. Çerez Politikası ve KVKK aydınlatma metinleri.